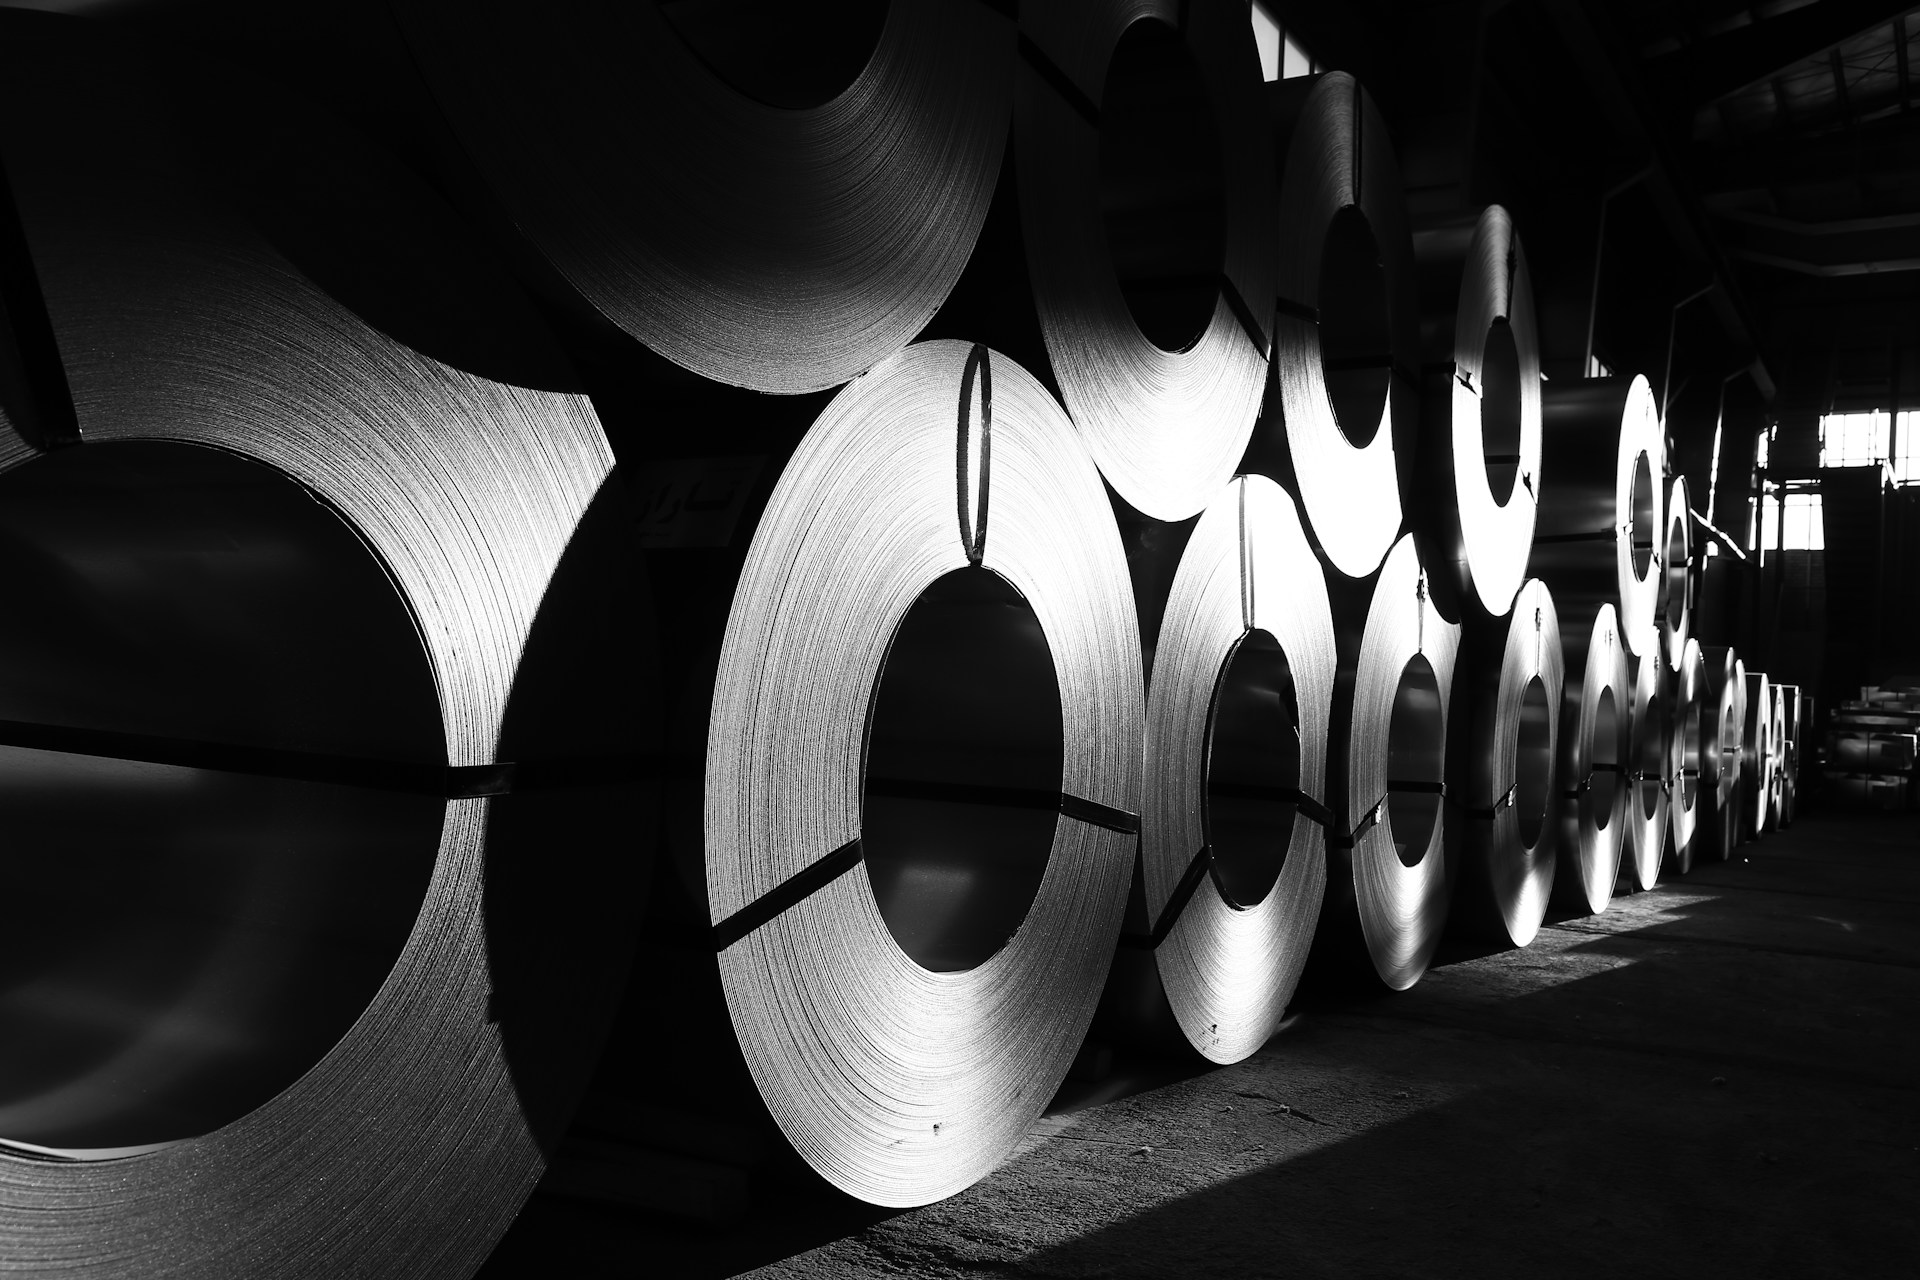
A small spring or clip can become costly when it fails in service. For manufacturers, the price of spring steel tells only part of the story. Delivery condition, processing and quality checks all influence whether components perform consistently. A poor choice can mean more scrap or costly rework.
1. Why does spring steel selection matter to manufacturers?
2. How do heat treatment and part design affect performance?
3. What should buyers check when sourcing spring steel strip?
4. When is AISI 1075 the right choice, and when is it not?
5. How can procurement reduce the total cost of components?
Why does spring steel selection matter to manufacturers?
A spring is designed to deform under a specified load and recover without permanent set. Even in a small clip, repeated movement can cause fatigue damage. Nominal steel strength alone says little about how a finished part will perform. High-carbon spring steels can be used for flat springs, retaining components and certain cutting tools. Appropriate heat treatment can provide hardness and wear resistance, but excessive hardness or damaged edges can increase the risk of cracking.
Batch variation can affect assembly fit, rejection rates and delivery schedules. For example, a stamped clip that is slightly too stiff may be difficult to install, while one that takes a permanent set may no longer hold its mating part securely. The selected steel must deliver consistent results with the manufacturer’s production process.
How do heat treatment and part design affect performance?
AISI 1075 is a high-carbon steel containing approximately 0.70–0.80% carbon, depending on the applicable specification. Carbon allows the steel to be hardened, while quenching and tempering influence the balance between hardness, strength and toughness. The final properties depend on more than the grade designation, including section thickness and processing conditions.
Manufacturers can buy softer strip for forming or strip already hardened and tempered. Softer stock may stamp or bend more easily before heat treatment; hardened strip avoids some steps but demands suitable tooling.
Heat treatment can introduce defects. Decarburisation can leave a softer surface layer, while oxidation or distortion can affect finish and dimensions. Under repeated flexing, edge defects can initiate fatigue cracks. Testing should cover the finished component rather than relying solely on the hardness of incoming material.
What should buyers check when sourcing spring steel strip?
A purchase specification should define grade, condition and dimensions. Thickness variation can noticeably change spring stiffness; width, flatness, finish and edge quality also affect stamping yields. For thin parts, rolling direction and slit-edge quality can affect cracking during forming; trial production should check both.
Grade names require care when purchasing across markets. The designation AISI 1075 spring steel is commonly cross-referenced with European C75S (1.1248), although their chemical composition limits are not identical. Buyers should verify the applicable material standard, delivery condition and inspection requirements before treating them as interchangeable.
EN 10132-4:2000, still cited in older catalogues for cold-rolled spring strip, was superseded by EN 10132:2021. Orders should identify the applicable edition, delivery condition and dimensional tolerances, together with the required inspection documentation.
When is AISI 1075 the right choice, and when is it not?
AISI 1075 can be suitable for relatively thin spring components, provided that the material condition and heat treatment meet the application’s requirements. It is not suitable for every design: thick sections or demanding fatigue conditions may require another grade, especially where through-hardening is difficult.
Corrosion is another limitation. Unlike stainless grades, high-carbon spring steel has limited resistance to moisture and aggressive chemicals. Coatings may help, but protection must be assessed for the actual environment, especially outdoors or during washdown. Joining and fabrication constraints are also important. High carbon content complicates welding and can raise cracking risks. If a design relies heavily on welded joints, the material and manufacturing method should be reviewed together before committing to production.
How can procurement reduce the total cost of components?
A lower price per tonne can be misleading if material variability increases scrap rates or inspection costs. Buying hardened strip when parts need extensive forming may add tooling costs. Purchasing, engineering and quality teams should agree on acceptance criteria before comparing quotes.
For repeat orders, it helps to record the approved material condition, dimensional tolerances, test evidence and any processing constraints. A sample run can expose issues with springback, punching quality or distortion before a full batch is produced. Measuring spring force at a specified deflection gives buyers and suppliers a clearer acceptance criterion than a general claim that the material is “spring quality”. Where multiple suppliers are involved, consistent documentation also makes substitutions easier to evaluate.
The most useful comparison is the cost of an acceptable finished part, including processing losses and any foreseeable rework, rather than the price of the incoming steel alone. Choosing spring steel with those costs in mind gives manufacturers a firmer basis for planning production and reducing avoidable quality problems.